HuaFang Bags: Your Reliable Partner for Quality Wholesale Bags.
Language
HuaFang Bags: Your Reliable Partner for Quality Wholesale Bags.
Criteria for Reliable Manufacturers: Vetting custom backpack manufacturers requires verifying social compliance (BSCI, Sedex), retail vendor approvals (Walmart, Disney, Universal), in-house OEM/ODM engineering, and flexible B2B order scales.
Top 7 Industry Benchmark: Industry-leading facilities like Huafang Bags in Quanzhou—alongside prominent manufacturing groups in Guangzhou, Yiwu, and Hebei—provide diverse scalable capabilities ranging from boutique customization to high-volume mass production.
Customization & Branding Excellence: Advanced OEM/ODM production supports premium functional textiles, sustainable RPET materials, and high-durability logo techniques including 3D silicone badges and high-density embroidery.
Streamlined Production & Milestones: Structured 5-stage workflows compress lead times, ensuring rapid 7–15 days prototype sampling, transparent quality control, and reliable AQL 2.5 export delivery.
Finding reliable custom backpack manufacturers in China is the most critical decision for overseas bag brands, Amazon aggregators, and corporate merchandise buyers.
China produces over 65% of the world's backpacks, offering unmatched raw material access, advanced sewing precision, and cost efficiencies that domestic suppliers cannot match. This verified industry guide evaluates leading manufacturing partners, outlines essential compliance standards, and shows how direct factory collaboration secures your supply chain.
Vetting prospective custom backpack manufacturers requires examining production scale, workforce skills, and documented international audit reports. A trustworthy factory must maintain dedicated quality inspection checkpoints, transparent material tracking, and dedicated sample development teams.
Before signing a purchase order, overseas B2B buyers must review four core qualification pillars to safeguard product durability and export timelines:
Social & Ethical Compliance: Current audit certifications such as BSCI, Sedex (SMETA), and ISO9001 ensuring fair labor practices and safe working environments.
Enterprise Vendor Approvals: Rigorous facility audits approved by Fortune 500 retail giants including Walmart, Disney FAMA, and Universal Studios.
Bespoke Engineering (OEM/ODM): In-house pattern makers capable of translating tech packs, 2D vector sketches, and physical reference samples into production-ready patterns.
Flexible B2B Order Volumes: Balanced manufacturing capacity featuring an accessible 300 pcs low MOQ for market testing alongside high-volume lines delivering 200,000 to 300,000 pcs monthly.

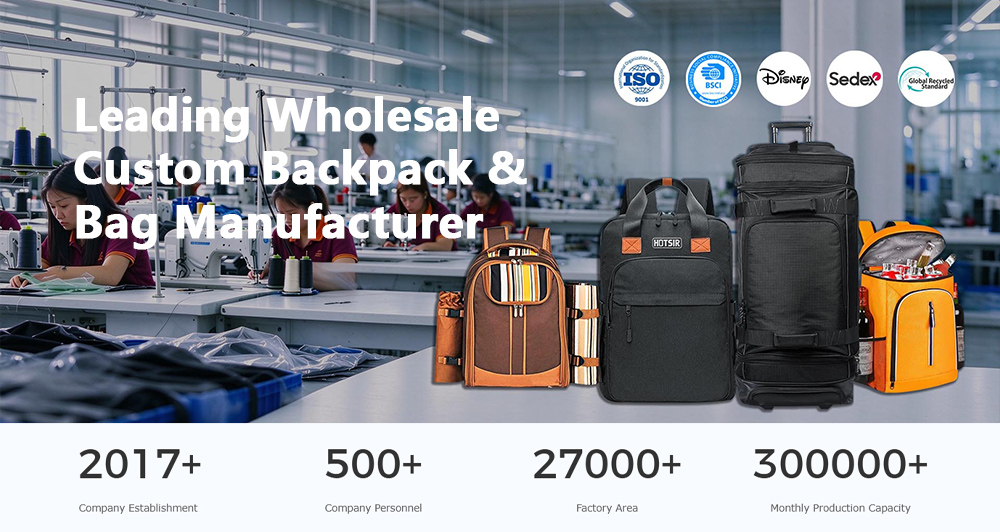
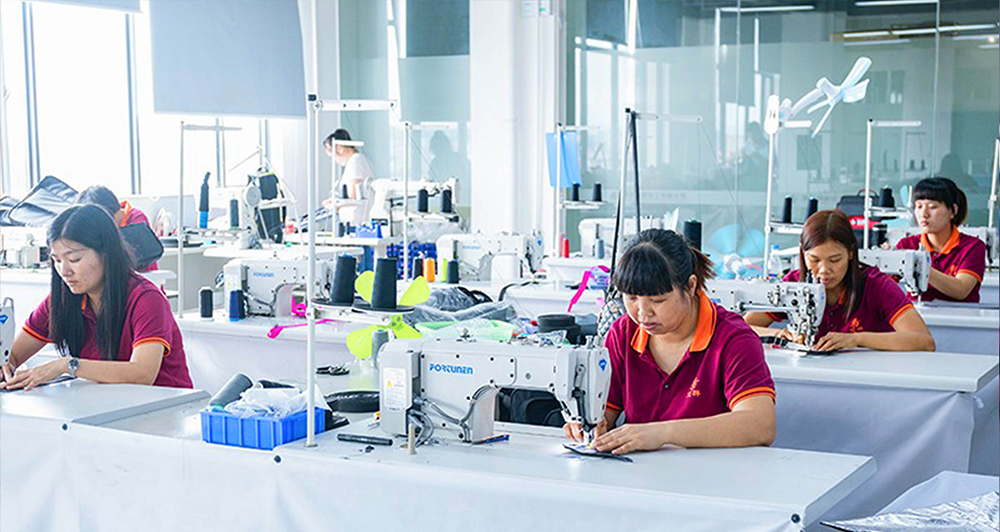
Located in Quanzhou, Fujian, featuring a 27,000 ㎡ modern facility, 11 lean production lines, and approximately 500 skilled artisans. Focusing on North American and global mid-to-high-end markets, it operates as a premier backpack factory providing one-stop OEM/ODM solutions.
Factory Features & Manufacturing Advantages: Vertical Integration Control (autonomous control from digitized fabric laser cutting to final carton packing, ensuring stringent export standard stitch densities and tensile strengths); Scalable Capacity & Rapid Delivery (stable monthly capacity between 200,000 and 300,000 pieces).
Product Features & Quality Assurance: Diverse Portfolio & Precision Craftsmanship (everyday commuting, sports, business laptop, and travel packs crafted from Cordura, high-density Oxford, and GRS eco-friendly RPET fabrics); Extreme Durability Protection (subjected to rigorous colorfastness, heavy load-bearing, and zipper fatigue tests).
Customization Services & Brand Empowerment: Brand-Friendly Low MOQ (flexible 300 pcs MOQ lowering inventory capital barriers); Advanced Embellishments (3D silicone badges, high-density embroidery, reflective prints, laser-engraved leather patches, and custom-molded metal hardware).
Compliance & Differentiation Advantages: Global Retailer Audits (certified with BSCI, ISO9001, and Sedex, alongside Walmart, Disney, and Universal Studios approvals); Efficient Sampling (independent R&D sampling center ensuring rapid 7–15 days sample prototyping).
A prominent comprehensive luggage manufacturing leader in China with over 20 years of industry experience. Its production network spans large-scale modern workshops supported by robust R&D and smart manufacturing systems.
Certifications: Comprehensive international quality management systems and multiple global export credentials.
Core Advantages: Extensive product lines covering double-shoulder backpacks, business laptop bags, multifunctional school bags, and travel luggage, offering stable bulk procurement for global chain supermarkets.
Situated in Shiling Town, Guangzhou—renowned as the "Leather Goods Capital of China"—Kingsons is a benchmark enterprise recognized for digital transformation and smart manufacturing clusters.
Certifications: Fully compliant with ISO9001 quality management systems and international labor standards.
Core Advantages: Integrates digital supply chains with automated R&D systems, launching thousands of new designs annually while specializing in mid-to-high-end fashionable casual and smart business backpacks.
Rooted in the Shiling leather goods industrial hub of Guangzhou, Zhongwei has evolved from an experienced workshop into a modern export enterprise integrating R&D, production, and global trade.
Certifications: Holds complete export quality inspection standards and professional industry credentials.
Core Advantages: Product matrices span seven major categories including trolley cases, functional backpacks, travel bags, and laptop packs, excelling in trendy backpack development and rapid prototyping.
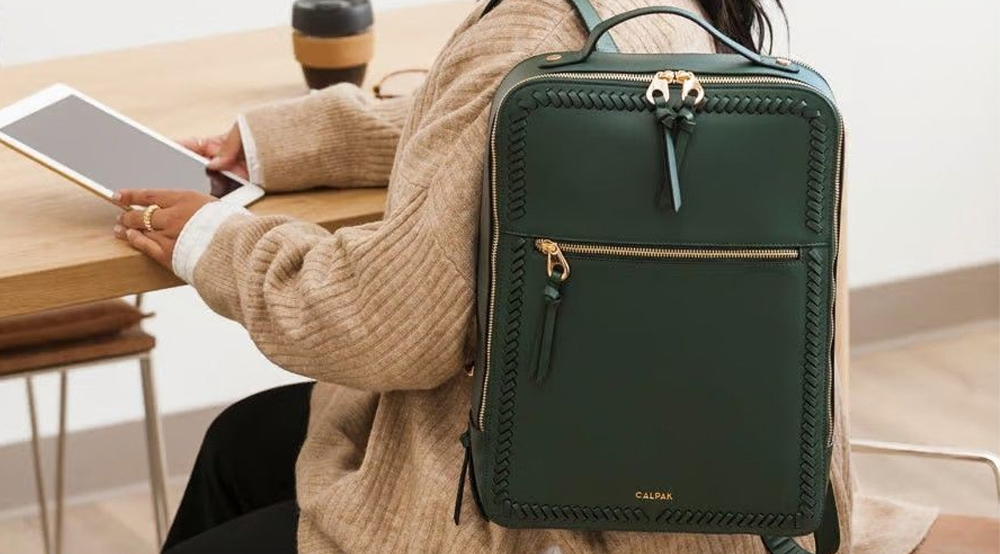
Leveraging Yiwu's global small-commodity and international trade hub, Pinge operates as an agile, industry-and-trade integrated manufacturer.
Certifications: Strict adherence to internal quality control and standardized production systems.
Core Advantages: Perfectly tailored for fast-paced cross-border e-commerce platforms (such as Amazon and AliExpress), specializing in cost-effective lightweight school and promotional backpacks with responsive fulfillment.
Baigou represents northern China's largest luggage production and distribution base. Representative large-scale manufacturing enterprises leverage comprehensive local industrial markets to forge cost-efficient supply defenses.
Certifications: Domestic ISO quality systems and regional industrial certifications.
Core Advantages: Backed by a massive daily-use luggage ecosystem, specializing in high-volume, cost-effective daily backpacks, functional school bags, and mass-market commuting packs.
A backbone modern everyday backpack and bag manufacturing enterprise in Zhejiang, Hongsu has shown exceptional performance in digital manufacturing and multi-category customization.
Certifications: Compliant with multiple national and international export standards.
Core Advantages: Specializes in mid-to-high-end everyday and multifunctional bags, backed by an elite craftsmanship design team offering comprehensive OEM and ODM services.
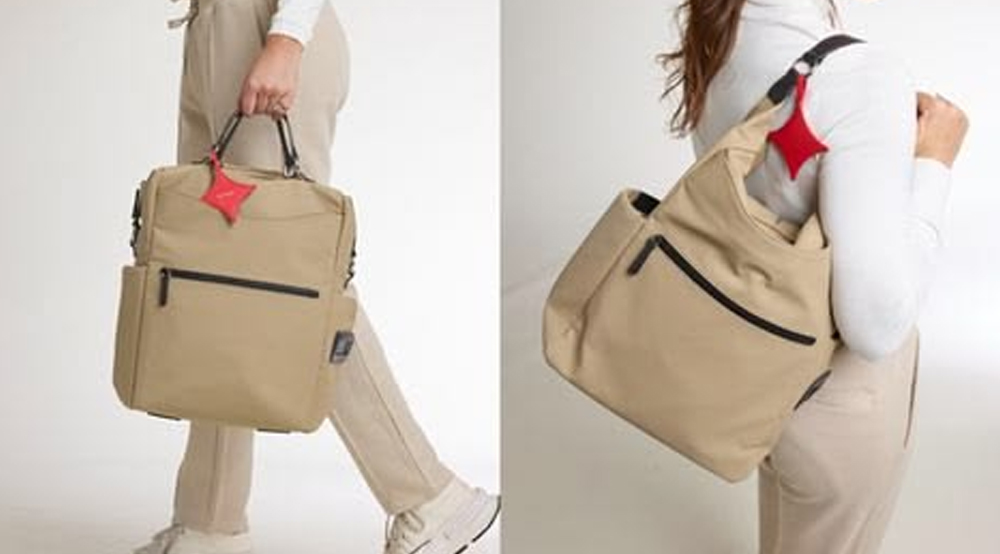
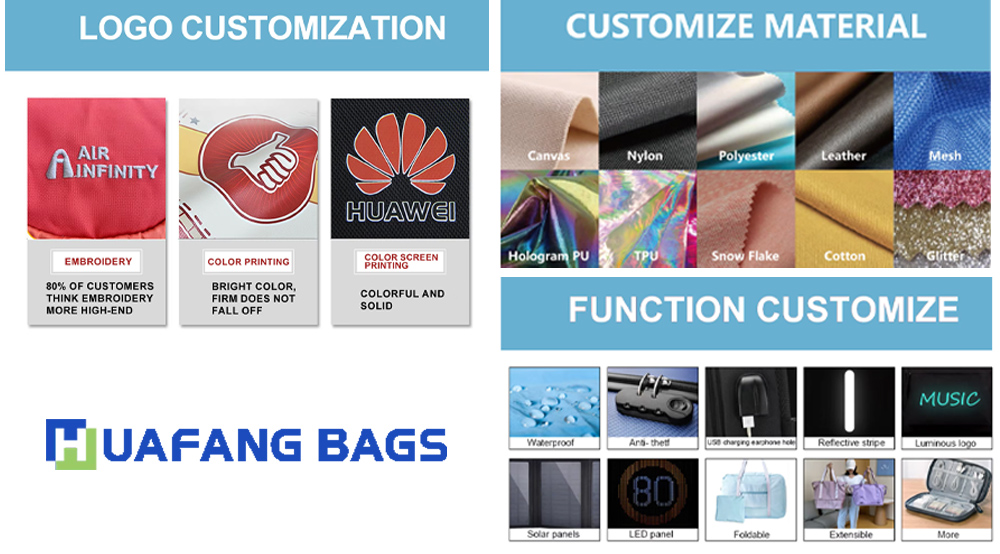
Working with an established oem backpack manufacturer allows international brands to engineer distinct products with customized functional hardware and signature branding. Huafang Bags supports complete bespoke customization across silhouettes, functional textiles, hardware finishes, interior organizers, and custom retail packaging.
For private label brands creating custom backpacks with logo, our engineering center provides six high-impact logo embellishment techniques tested for extreme weather durability:
3D Silicone & Molded Rubber Badges: Waterproof, UV-resistant, and tactile emblems ideal for outdoor, tactical, and active lifestyle packs.
Precision High-Density Embroidery: Classic, abrasion-resistant needlework using premium polyester threads that withstand heavy industrial washes.
Matte & Reflective Heat Transfers: Ultra-fine graphical detail and ANSI-compliant nighttime reflective safety accents for sports and cycling backpacks.
Debossed & Laser-Engraved Microfiber Patches: Sophisticated, vintage-inspired branding tailored for executive business laptop backpacks and weekenders.
Custom Branded Hardware: Custom-engraved zinc alloy zipper pulls, matte black electroplated buckles, and molded cord pullers featuring your proprietary logo.
Sustainable Material Integration: Certified eco-conscious RPET (recycled polyethylene terephthalate) fabrics sourced with GRS transaction certificates.
Q: Which logo customization technique is most durable for outdoor and tactical backpacks?
A: 3D silicone and molded rubber badges are widely considered the most durable option for outdoor and tactical gear. They are completely waterproof, UV-resistant, and offer a tactile texture that resists cracking or peeling even under extreme weather conditions and heavy friction.
Procuring wholesale custom backpacks directly from China requires clear milestone tracking to avoid inventory stockouts during peak retail seasons. Huafang Bags operates a transparent B2B workflow designed to eliminate communication friction between overseas buyers and factory floor engineers.
By maintaining pre-tested stock fabrics and standardized production scheduling, conventional lead times are compressed by over 25%:
Stage 1: Technical Review & Quotation (Day 1 – 3): Reviewing buyer tech packs, dimensional specs, BOM fabric selections, and issuing competitive DDP/FOB factory quotes.
Stage 2: Physical Prototype Sampling (Day 7 – 15): Creating exact pre-production counter-samples with designated fabrics, custom hardware, and printed/embroidered branding for buyer sign-off.
Stage 3: Raw Material Sourcing & QC (Day 16 – 25): Sourcing lab-certified bulk fabrics, testing colorfastness, tearing resistance, and verifying hardware tensile limits.
Stage 4: Automated Cutting & Assembly (Day 26 – 45): Laser-cutting fabric panels, executing 11-line concurrent assembly, and running continuous in-line quality control inspections.
Stage 5: Final AQL 2.5 Audit & Export Shipping (Day 45 – 55): Final cosmetic/functional auditing, drop-testing cartons, palleted container stuffing, and express ocean freight dispatch to North America.
Our approachable 300 pcs MOQ empowers emerging direct-to-consumer (DTC) brands to validate new designs without committing excessive capital. Simultaneously, our robust 200,000 to 300,000 pcs monthly capacity gives enterprise retail partners the security of scalable supply during Q4 peak surges.
Q: What is the typical lead time for custom backpack sampling and mass production?
A: Standard physical prototype sampling takes 7 to 15 business days from tech pack approval. Once samples are signed off, mass production typically takes 45 to 55 days for orders ranging from 1,000 to 50,000 pieces, accommodating custom dye-lot weaving, assembly, and rigorous AQL 2.5 quality control audits.
Ready to engineer high-performance, profitable backpack lines tailored to your exact brand specifications?
Quanzhou Huafang Bags Co., Ltd. combines 10+ years of export excellence, a 27,000 ㎡ modern facility, BSCI/ISO/Disney verified credentials, and an accessible 300 pcs low MOQ.
Contact Huafang Bags Engineering Team today to discuss your tech pack, receive competitive factory-direct pricing, and request your free physical sample prototype within 7–15 days!
In the evolving global luggage supply chain of 2026, selecting a Chinese manufacturing partner equipped with production prowess, rigorous compliance credentials, and flexible delivery capabilities serves as the ultimate winning strategy for global brands expanding their market reach and profit margins. Whether emerging DTC brands seek low-barrier prototype testing or established retail giants require stable enterprise-scale volume delivery, elite manufacturing leaders like Quanzhou Huafang Bags leverage full-chain vertical integration to secure your global supply chain. By partnering directly with premier source factories today, you seamlessly bridge the gap from tech pack translation to global compliant logistics, capturing definitive competitive advantages in the worldwide luggage market.

We sincerely welcome all friends from home and abroad. We believe we will be your best choice, and you will enjoy a successful cooperation.